|
|
Why is a five axis CNC machine tool linked to five axes instead of six axes?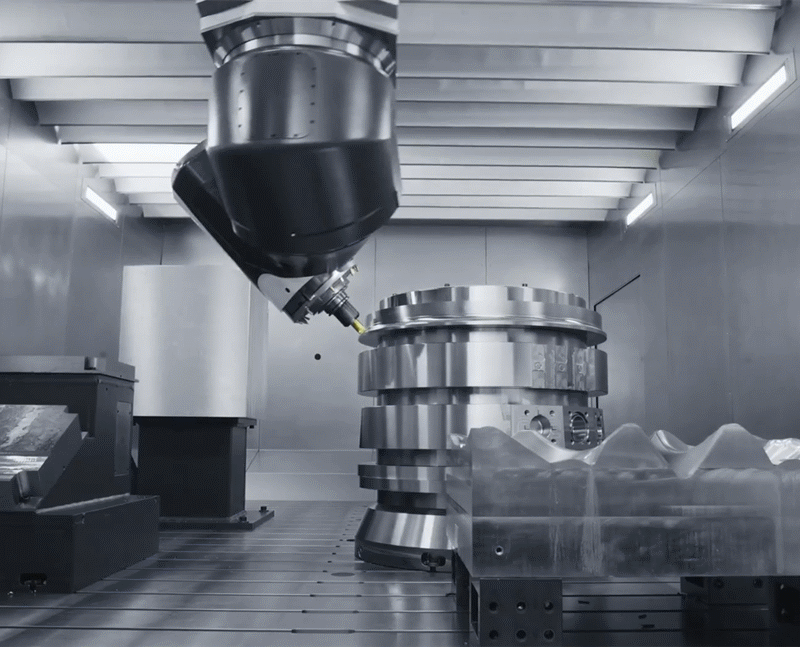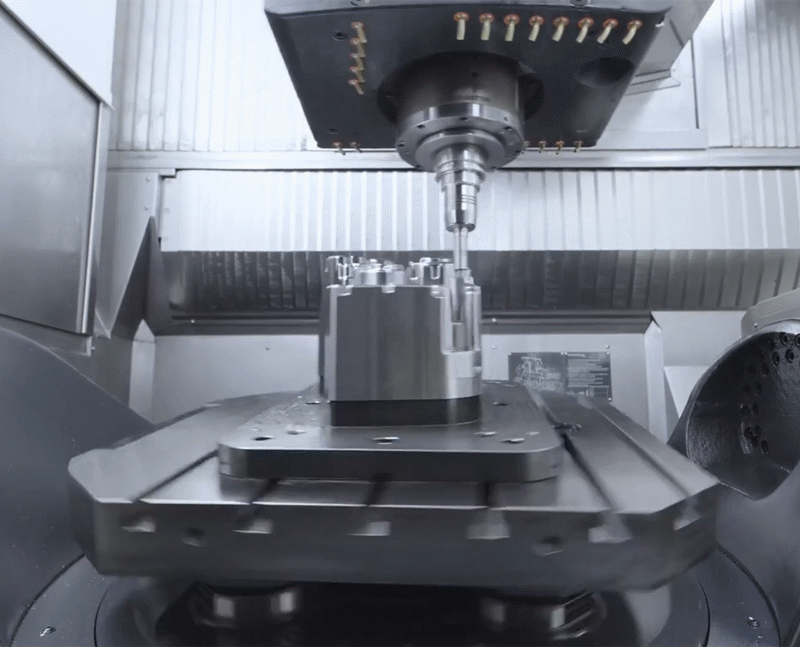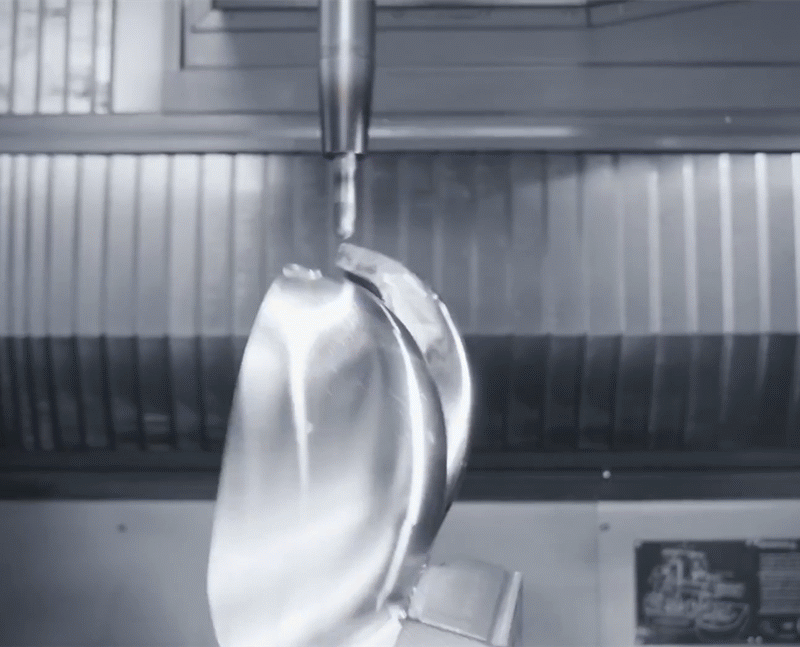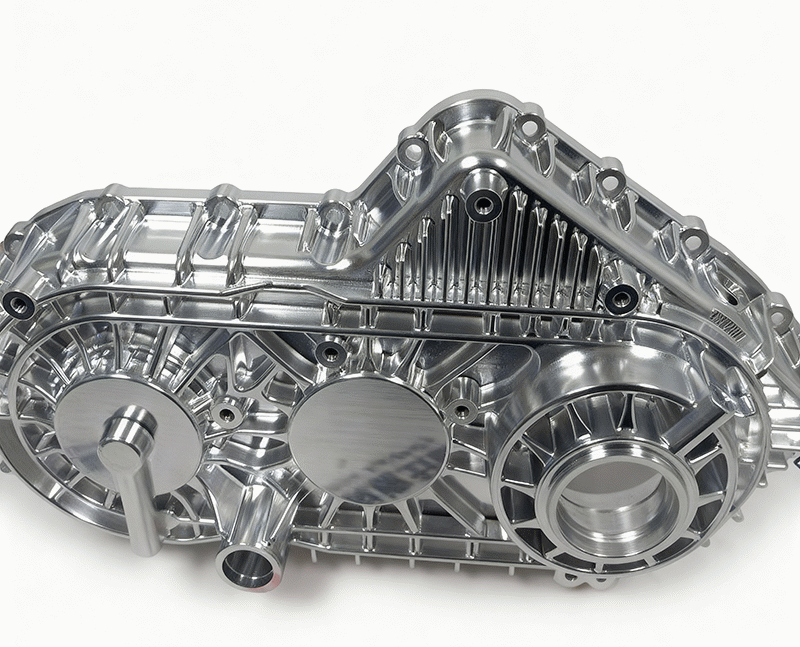  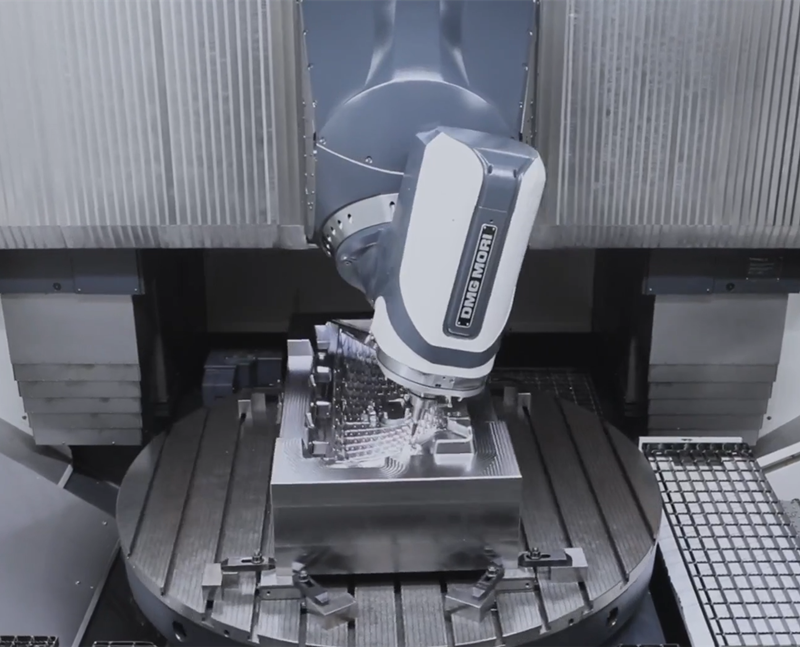  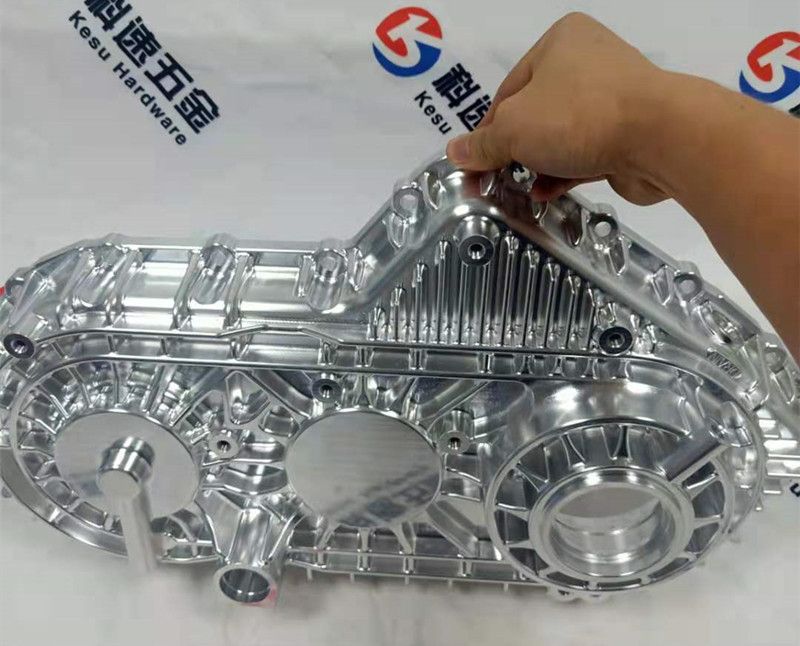 Why is a five axis CNC machine tool linked to five axes instead of six axes?The fundamental reason why machine tools can achieve arbitrary angle machining is that the tool or probe can approach the workpiece in any direction. And five axis linkage is the least linkage axis, which can achieve machining at any angle.
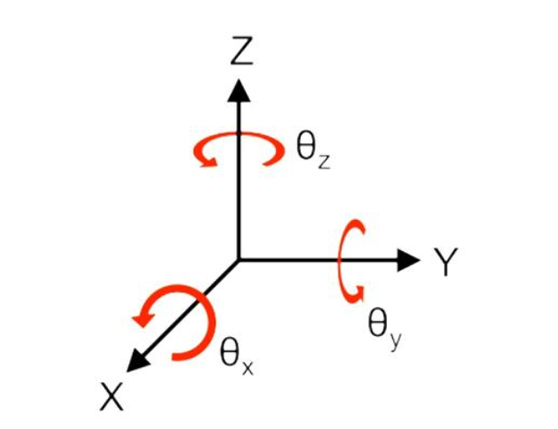
Five-axis Simultaneous Machining Product description The fundamental reason why machine tools can achieve arbitrary angle machining is that the tool or probe can approach the workpiece in any direction. And five axis linkage is the least linkage axis, which can achieve machining at any angle. Usually, only five axes are adaptive. This is because the fewer the linkage axes, the simpler and more compact the machine tool structure, making it easier to ensure the dynamic and static stiffness of the machine tool. Dynamic stiffness and static stiffness are crucial for machine tools that require very high precision. There is a thought that may remain in our brain. In 3D space, an object has 6 degrees of freedom (DF). As shown below.
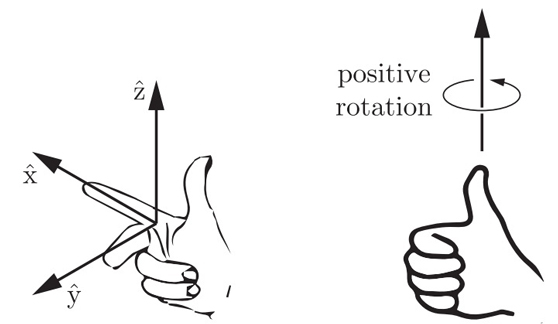
Six DFs in 3D Space This is a right-handed coordinate system. These 6 degrees of freedom (DF) are three linear degrees of freedom along the X, Y, and Z axes; And three degrees of freedom for rotation around the X, Y, and Z axes. The positive direction of rotation satisfies the right-hand spiral rule. As shown below.
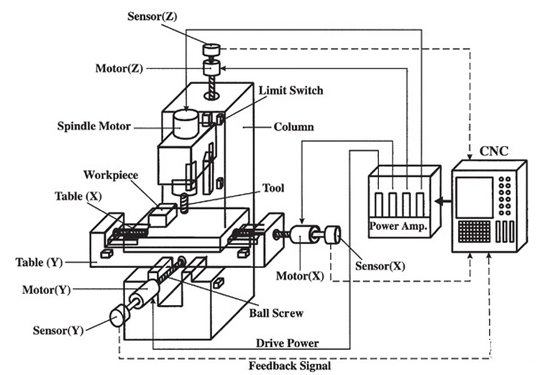
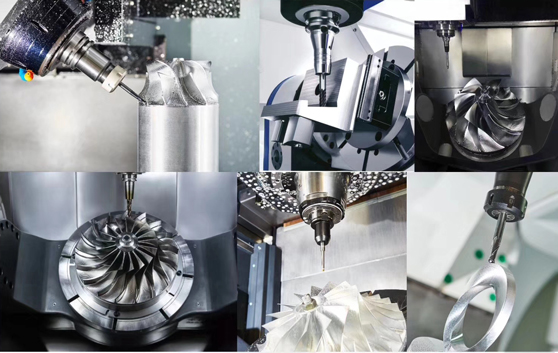
Right-handed coordinate system Due to the influence of this concept, we may assume that machine tools require 6 degrees of freedom or 6 axes to achieve machining in any direction. In fact, objects have 6 degrees of freedom, which does not mean that machine tools need to be composed of 6 axes to achieve machining at any angle. This is the key to this problem. When traditional three-axis machine tools machine workpieces composed of complex surfaces or holes in multiple directions. We need to use special fixtures and make many changes in the process to ensure that the tool can contact the workpiece from any direction. When using a five axis linkage CNC machine tool, high-speed and high-precision machining of complex shaped workpieces can be achieved with just one clamping. That is to say, the tool or probe can approach the workpiece in any direction, which is the key to enabling machine tools to achieve machining in any direction. Machine tools achieve machining by controlling the position and orientation of cutting tools or probes. Therefore, the key point or premise is how to describe the position and posture of the tool or probe. Three axis CNC machine tool During the machining process of a three-axis CNC machine tool, the position of the cutting tool or measuring head varies, but its posture is fixed. For example, when machining with a typical vertical three-axis machine tool, the tool direction is in the positive Z-axis direction. The position and orientation of the cutting tool or measuring head can be determined based on the linear axis coordinates of X, Y, and Z.
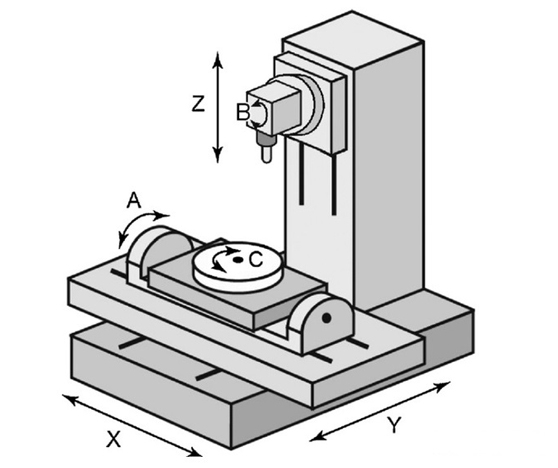
Three-axis machine Five axis CNC machine tool Under normal circumstances, a 5-axis machine tool adds 2 rotational axes on top of a 3-axis machine tool. Usually, the A, B, and C axes represent the rotation axes around the X, Y, and Z linear axes. A 5-axis machine tool consists of any two axes, A, B, and C.
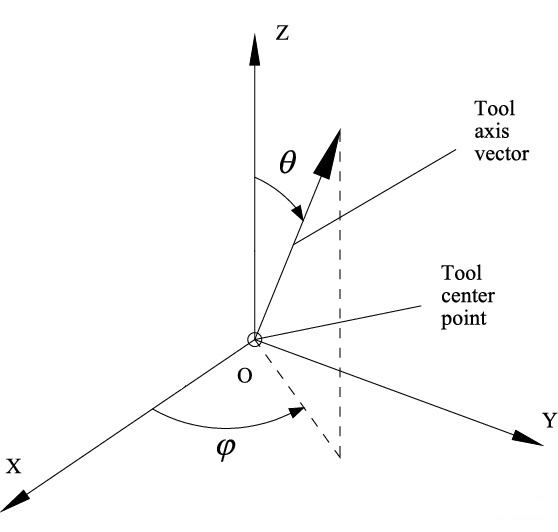
Five axis machine Please note that the above figure only represents the relationship between the rotation axis and the linear axis, and is not the actual configuration of a 5-axis machine tool. In fact, the rotation axis of a 5-axis machine tool consists of two axes, A, B, and C. For example, A and B, or A and C, or B and C. Due to the presence of these two rotation axes, the position and orientation of the tool or probe may change during the five axis machining process. Obviously, after determining the reference point on the spindle, the position of the tool or probe can be determined through the linear axes X, Y, and Z. Of course, in practical operation, it is also necessary to consider the influence of the distance from the rotation center to the cutting edge and the rotation angle. But what about the posture of the tool or probe? In order to describe the posture of the tool or probe during the machining or testing process, the concept of tool axis vector is derived. The blade axis vector is a three-dimensional unit vector (i, j, k). Each element corresponds to the projection value of the unit vector in the direction of the tool axis, which is projected on the linear axes X, Y, and Z.
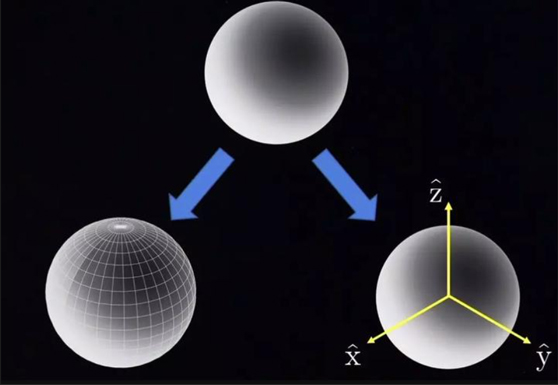
Tool axis vector Since the knife axis vector is a unit vector with a modulus length of 1, all possible positions of the vertices of the knife axis vector in space form a sphere with a radius of 1. The direction of any tool axis vector can be obtained by rotating the vector in space around two non collinear axes. This may sound abstract, but there is a good example in our daily lives. Longitude and latitude, also known as φ and θ in the above figure. We can determine any position on the Earth's surface through longitude and latitude. Longitude and latitude consist of only two coordinates, which can be described by the angle between two perpendicular axes of rotation. In the following figure, when determining the position of a point on a sphere, each point corresponds to a tool axis vector, which can be described using two coordinate systems. 1. Use the left-hand spherical coordinate system, also known as the explicit expression of spherical coordinates. That's longitude and latitude, which are composed of two coordinates, so they correspond to two degrees of freedom because longitude and latitude are independent of each other. 2. Use the XYZ system on the right, also known as implicit expression. Contains three coordinates, but still corresponds to two degrees of freedom. Because these three coordinates contain an implicit constraint. x^2+y^2+z^2=1
Spherical coordinate system (left) and XYZ system (right) Therefore, the rotation angle of the two rotation axes can describe a determined position on the sphere. The projection values of the determined spherical position to the front X, Y, Z are used to describe the tool or probe posture as the tool axis vector (i, j, k). In this way, a one-to-one correspondence is established between the rotation angle of the two axes and the tool axis vector. In actual five axis machining, the numerical system will obtain the rotation angles of each of the two rotation axes According to the numerical program's tool axis vector and kinematic relationship. Then the system will control these two rotation axes and three linear axes, combined with the coordinates of the linear axes. So as to move the tool or probe to the predetermined position and posture. A popular but not very rigorous method is to add two more rotation axes to a three-axis machine tool, which can control the tool to approach the workpiece in any direction and achieve the machining of any complex surface. If the machine tool adds two rotating axes on the basis of a 3-axis machine tool and applies CNC system, servo system, and RTCP (rotating tool center point), it can achieve 5-axis linkage machining, which can be called a 5-axis linkage CNC machine tool.
RTCP Why don't 5-axis machines use more linkage axes? On the one hand, 5 linkage axes are the minimum number of linkage axes required to achieve arbitrary angle machining. We explained the reason in the previous paragraph. On the other hand, typically only five axes are used. Because the fewer the linkage axes, the simpler the machine structure, the greater the impact force, and the easier it is to ensure the dynamic and static stiffness of the machine. Dynamic stiffness and static stiffness are crucial for high-precision CNC machine tools. But this will not affect the birth of higher axis coupled motors. The production of such machine tools is mainly to meet obstacle avoidance or special optimization objectives. Such as minimum motor power. In order to meet these special requirements, there are too many cases where dynamic stiffness and static stiffness are sacrificed to increase the linkage axis. Why do five axis machine tools only need five linked axes to achieve machining at any angle? The key is that only two degrees of rotational freedom are needed to express the tool axis vector in any direction. Contact us to learn more about 5-axis machining.
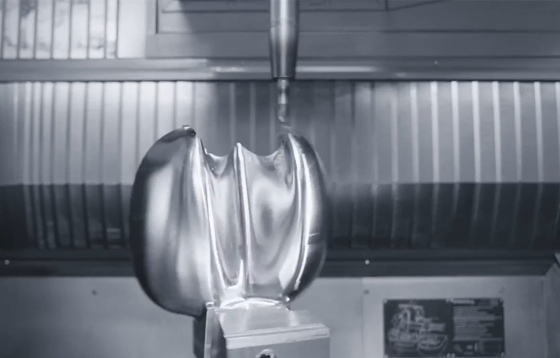
5-axis simultaneous control
|